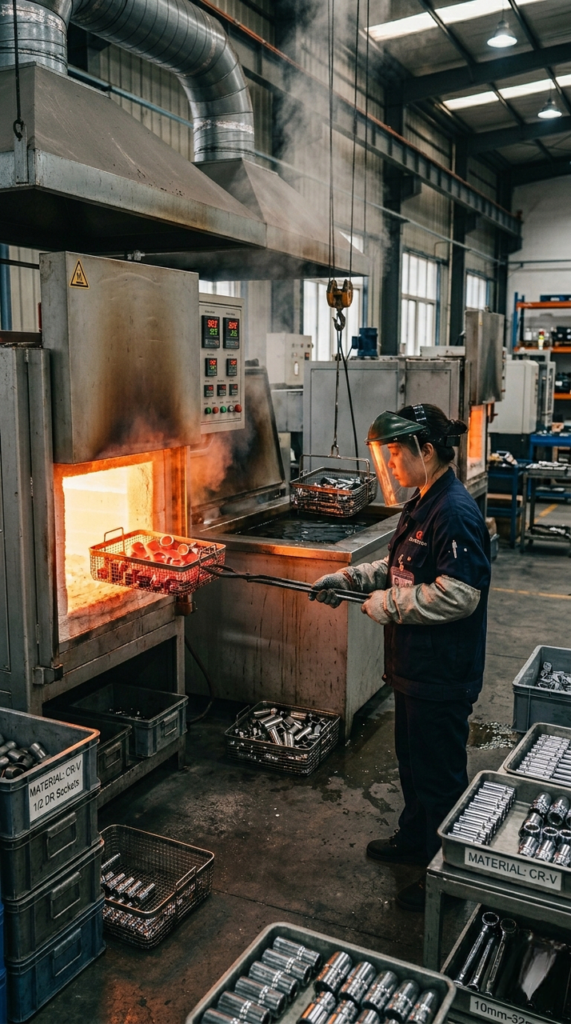
The heat treatment process of socket tools centers on quenching and tempering, aiming to strike a balance between hardness and toughness. Mainstream processes are classified into the following three categories based on their applications and materials:
- Ordinary manual socket: carburized/tempered treatment
· Process: Mostly carburizing + quenching + low-temperature tempering are adopted. For materials like 45 steel or 40Cr, surface carburizing is carried out first, followed by quenching at approximately 820-880℃ and tempering at 160-320℃.
· Effect: The surface is wear-resistant and the core has good toughness, with the final hardness usually ranging from HRC 34 to 48. - Pneumatic/Professional Socket: Vacuum Heat Treatment
· Process: Heat quenching and tempering under vacuum to achieve no oxidation, no decarburization, and maintain the original metallic color.
· Effect: Bright appearance, high fatigue strength, and moderate hardness to withstand impact, typically around HRC 40-48. - Special Performance Processes
· Forge heat quenching (utilization of residual heat): Direct quenching is carried out using the high temperature after forging (about 900-1000℃), followed by low-temperature tempering. This method is energy-saving and results in high strength.
· Induction quenching (local strengthening): High-frequency heating is applied to the force-bearing parts of the sleeve (such as the four-way drive head) and then rapidly cooled.
· Carbon-nitrogen co-penetration: Nitrogen is introduced on the basis of carburizing to further enhance wear resistance and rust prevention.
Leave a Reply